I. Green Material, Solid Foundation for Environmental Protection
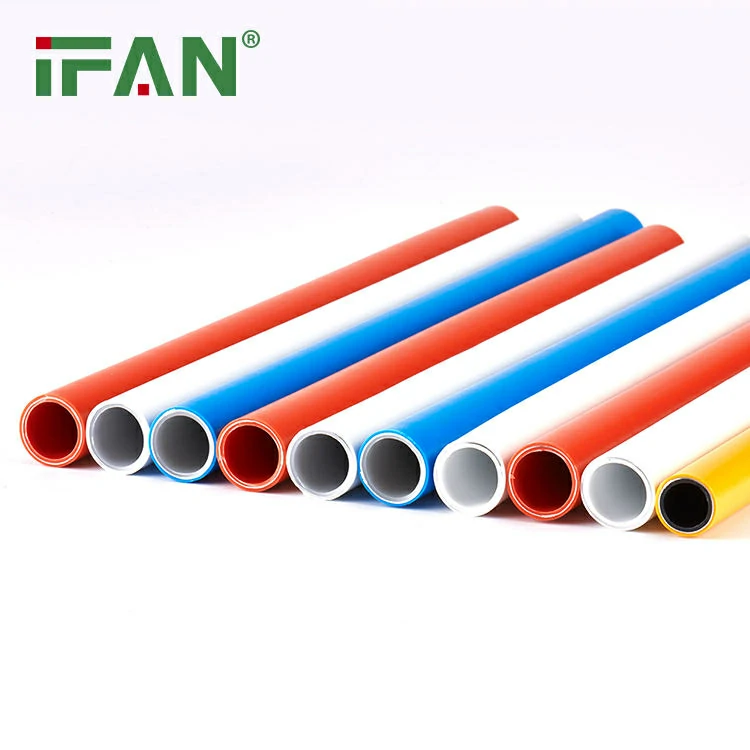
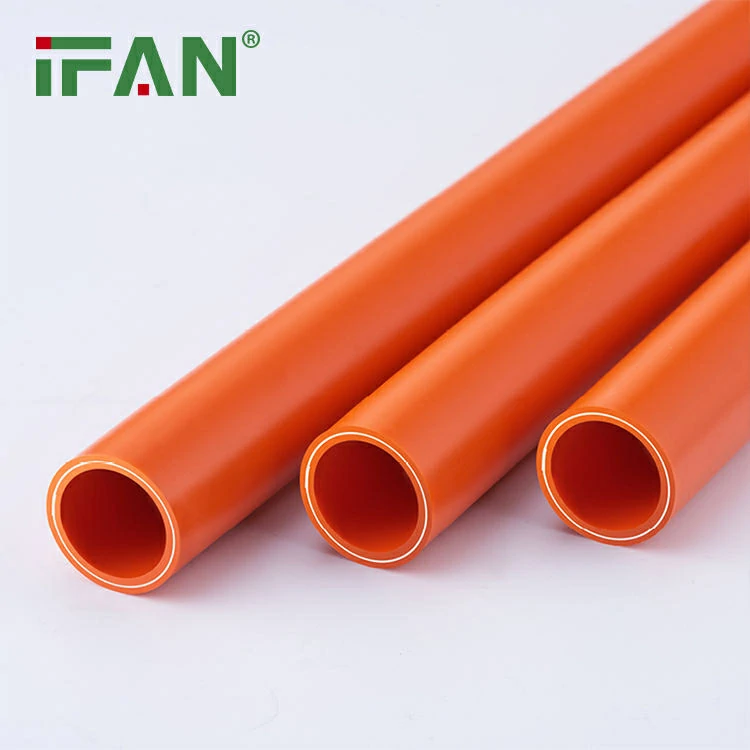
PPH Pipe, or Polypropylene Homopolymer Pipe, is crafted from high-grade polypropylene homopolymer material. This material stands out for its non-toxic, odorless nature and full recyclability, aligning perfectly with the modern industry’s pursuit of green production and sustainable development. During production, PPH Pipe generates no harmful emissions, and in use, it poses no risk of contamination to the transported fluids. Its compliance with international environmental standards ensures a solid foundation for environmentally conscious enterprises.
II. Exceptional Performance, Tackling Complex Conditions
- Superior Corrosion Resistance: PPH Pipe excels in resisting a broad range of acids, alkalis, and salts, ensuring stable performance even in corrosive environments. This feature makes it an ideal choice for chemical and environmental industries.
- High Temperature Tolerance: Capable of maintaining stability across a wide temperature spectrum, PPH Pipe ensures efficient fluid transmission even under high-temperature conditions, making it invaluable in petrochemical and other industries where heat is a factor.
- Lightweight yet Strong: Combining lightweight with exceptional strength and flexibility, PPH Pipe simplifies installation and reduces transportation costs while withstanding significant pressure and impact.
- Low Fluid Resistance: With a smooth interior, PPH Pipe minimizes fluid resistance, enhancing transmission efficiency and reducing energy consumption. This attribute is particularly advantageous in municipal water supply, agriculture irrigation, and building drainage systems.
III. Versatile Applications, Meeting Diverse Needs
The versatility of PPH Pipe is unmatched, catering to virtually all industries requiring fluid transportation. From the chemical sector, where it handles corrosive media, to the food industry, where its non-toxic properties make it suitable for food-grade piping, PPH Pipe proves its worth. It also finds application in the pharmaceutical industry, adhering to the stringent purity and cleanliness standards demanded by pharmaceutical manufacturers. Furthermore, its presence in municipal water supply, agricultural irrigation, and building drainage underscores its broad appeal and adaptability.
IV. Simplified Installation & Maintenance, Enhancing Efficiency
Installing PPH Pipe is a breeze, thanks to its lightweight design and variety of connection methods, including hot-melt and electrofusion joints, eliminating the need for complex welding processes. This not only shortens installation time but also lowers overall project costs. Maintenance is equally straightforward, requiring periodic checks for tight connections and signs of wear or aging. Should any issues arise, repairs or replacements can be swiftly executed, ensuring uninterrupted pipeline operation.
V. Green Philosophy, Shaping the Future of Industry
As global awareness of environmental protection intensifies, green production and sustainable development have become paramount. PPH Pipe, with its eco-friendly material, pollution-free production process, and recyclability, embodies these principles. Its commitment to environmental stewardship positions it as a forward-thinking solution for industries seeking to reduce their carbon footprint and contribute to a greener future.
VI. Technological Innovation, Driving Industry Progress
PPH Pipe’s evolution is fueled by continuous technological advancements and product upgrades. By investing in cutting-edge production equipment and partnering with research institutions, manufacturers ensure PPH Pipe remains at the forefront of innovation. These efforts not only enhance production efficiency and product quality but also foster the development of new materials and technologies to meet evolving market demands.